WeizhenInternational Sales Request a quote

02Products

Rotating, pressure-retaining and corrosion-facing castings.

From decanter bowls and seven-metre roll shells to gas turbine casings, volutes and valve bodies. Every part is made to the customer’s drawing, in the alloy and delivery condition the duty calls for.

11 component families in 3D100 to 15,000 kg casting weightOEM and ODM to drawing

Drag to rotate

Schematic model, not to scale

Delivery condition

Centrifugal casting

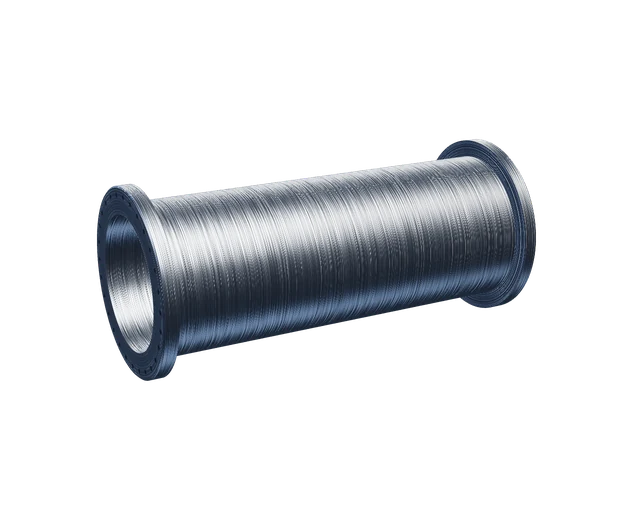
Cylindrical bowl for decanter centrifuges

The rotating shell at the heart of a decanter centrifuge, cast in one piece in duplex stainless steel. The manufacturer was a main drafter of the Chinese machinery standard for this component, JB/T 11874-2014.

Process
Centrifugal casting
Typical alloys
Duplex 2205 (EN 1.4462, UNS S32205 / S31803), duplex 2304 (EN 1.4362), super duplex 2507 (EN 1.4410); austenitic 304 and 316
Casting weight
100 to 1,500 kg
Maximum size
Ø 1,600 mm × 4,200 mm length
Dimensional tolerance
CT9 to CT12
Surface, as cast
Ra 12.5 to 50 µm
Surface, machined
Ra 0.8 to 6.3 µm
Heat treatment
Annealing, normalising, quenching or tempering
Delivery condition
As cast, rough machined or finish machined
Used in
Decanter centrifuges, pusher centrifuges, disc separators
Inquire about this part

Source: manufacturer’s published data, November 2026. Sizes and weights are published maximums or ranges, not stock dimensions. Material standards referenced: GB, ASTM, AISI, EN, DIN, BS, JIS, NF, AS, AAR.

2.1Full product range

Everything the foundry lists, by field of use.

All parts are made to order. If your component is not named here but is a stainless or special-alloy casting below fifteen tonnes, it is probably within range.

01 Centrifugal

Separation technology

  • Cylindrical bowls for decanter centrifuges
  • Conical bowls for decanter centrifuges
  • Duplex bowl sets
  • End hubs and head walls
  • Finish-machined end hubs
  • Scroll conveyors
  • Pusher centrifuge drums and baskets
  • Screw baskets for centrifuges
  • Separator drums

02 Sand and 3D print

Pumps, compressors and evaporators

  • Duplex multi-stage pump volutes
  • Volutes for MVR evaporators
  • Compressor volutes
  • Pump impellers
  • Rotors for pumps and compressors

03 Sand

Valves

  • Stainless steel valve bodies
  • Duplex stainless steel valve bodies
  • Valve cores

04 Centrifugal and sand

Pulp and paper

  • Suction roll shells
  • Duplex paper pulper impellers
  • Stainless steel pulper impellers

05 Centrifugal and sand

Power generation

  • Gas turbine outer casings
  • Gas turbine stator rings
  • Gas turbine diffuser casings
  • Hydro turbine runners
  • Deflectors for hydroelectric power
  • Nozzle covers for hydroelectric power

06 Centrifugal and sand

General engineering

  • Pipes, tubes and cylinders
  • Sleeves and liners
  • Bushings and seal rings
  • Heat-resistant steel gratings

2.2Delivery conditions

Supplied at the stage that suits your own machining.

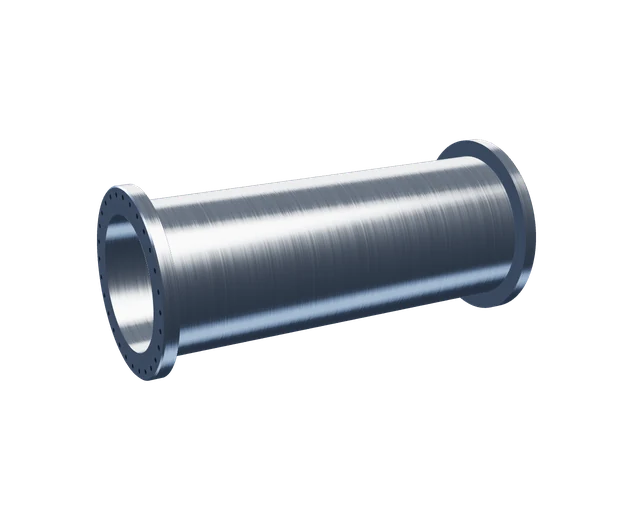
Schematic model of an as-cast shell

A

As cast

Supplied with machining allowance on functional surfaces. Dimensional tolerance CT9 to CT12, surface Ra 12.5 to 50 µm.

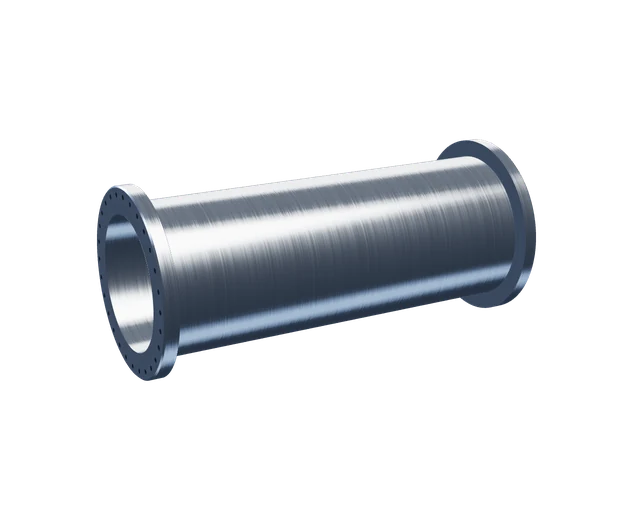
Schematic model of a rough-machined shell

B

Rough machined

Turned and bored to remove the casting skin and the bore layer, leaving finishing stock for your final operations.

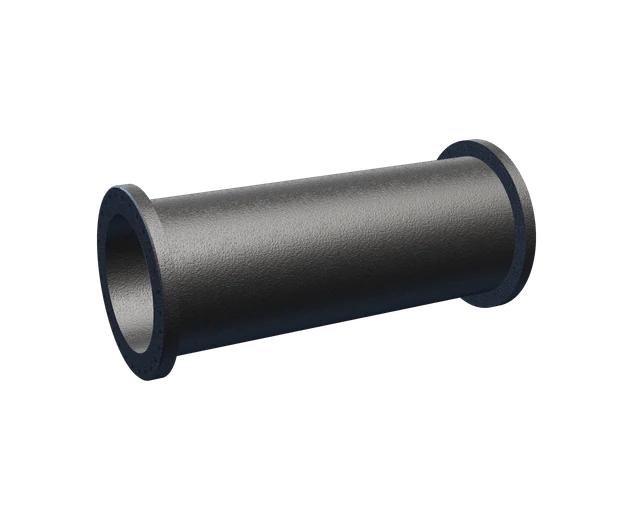
Schematic model of a finish-machined shell

C

Finish machined

Machined to drawing in house on CNC lathes, gantry mills and boring machines. Machined surfaces Ra 0.8 to 6.3 µm.

Next step

Send the drawing.
We return a manufacturing route.

Share geometry, alloy and duty. The foundry’s engineers review every inquiry for the casting process, heat treatment, machining condition and inspection scope that fit the part.